Stainless Steel Cutlery Polishing Process Consistency for OEM and Bulk Production
Stainless Steel Cutlery Polishing Process Consistency for OEM and Bulk Production
The final appearance of stainless steel cutlery depends heavily on the polishing process. Two spoons made from the same material and formed with the same tooling can look different if their polishing sequences, abrasive conditions or finishing methods are inconsistent. For importers, distributors and private label brands, these differences may become more noticeable when products are displayed together in a retail set or supplied across multiple production batches.
Polishing consistency is therefore more than a cosmetic concern. It affects how a cutlery collection reflects light, how decorative details appear, how surface marks are removed and how reliably the approved finish can be reproduced during bulk manufacturing.
Homefelt factory supplies stainless steel knives, forks, spoons and coordinated cutlery sets for B2B customers. By defining finishing requirements early and monitoring the process throughout production, buyers and manufacturers can reduce avoidable variation between samples and bulk orders.
Why the Polishing Sequence Matters
Stainless steel cutlery may undergo several surface preparation and finishing operations after forming. Depending on the design and required finish, these can include grinding, abrasive polishing, intermediate finishing, buffing and final cleaning.
Each stage has a specific purpose. Earlier operations may remove forming marks or refine the surface, while later stages help establish the requested appearance. If a later operation is expected to compensate for an inconsistent earlier stage, the result may become less predictable.
For example, deep marks left during grinding may require additional material removal to reduce their visibility. Excessive correction can change an edge, soften a decorative line or create differences in thickness and profile. A controlled sequence helps maintain the intended shape while achieving the required surface quality.
The exact process depends on the product design, stainless steel grade, initial surface condition and finish specification. A mirror-polished spoon and a brushed table knife should not automatically follow identical finishing procedures.
Matching the Polishing Method to the Required Finish
Before production begins, buyers should identify the intended finish using an approved physical sample, clear photographs and, where appropriate, a written surface specification.
Mirror Finish
A mirror finish is designed to create a highly reflective surface. It can emphasize the overall shape of a spoon bowl or handle, but it may also make fine scratches, cloudy areas and inconsistent reflections easier to notice.
To maintain a consistent appearance, the factory needs to control the progression from surface preparation to final polishing. The buyer should also define how the finished piece will be evaluated, because lighting and viewing angle can influence the perceived reflection.
Satin or Brushed Finish
A satin finish typically has a softer reflection, while a brushed finish may contain a deliberate directional grain. The direction, density and visual uniformity of that grain are important parts of the design.
Polishing in inconsistent directions can create visible differences between pieces. A clear finish reference should indicate which surfaces receive the brushed treatment and how the grain should run along the handle or head.
Decorative and Mixed-Finish Designs
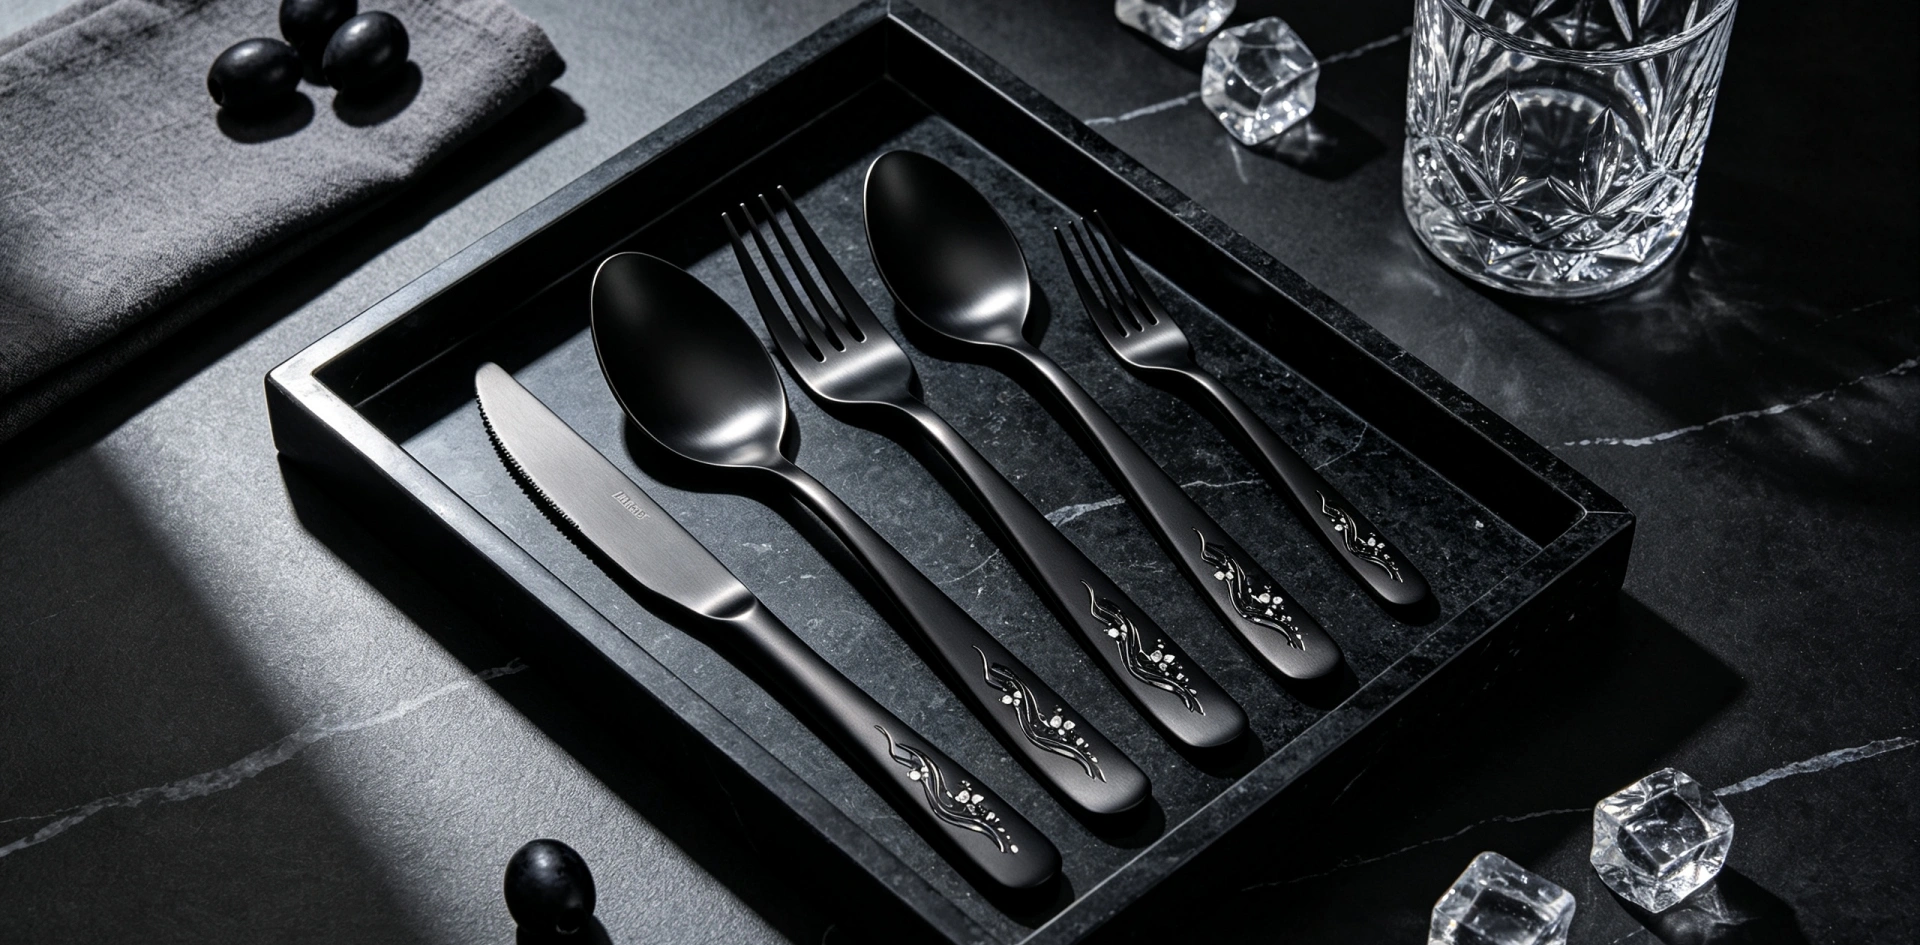
Some stainless steel flatware designs combine polished areas with brushed sections, patterned handles or other decorative details. In these cases, process control must address both the quality of each finish and the boundary between them.
If a decorative transition is not clearly defined, polishing may blur a line or create an inconsistent visual border. Product drawings and approved samples can identify the areas that require separate finishing treatment.
Abrasive Selection and Process Control
Abrasive materials and tools influence how quickly surface marks are removed and what kind of finish is produced. The appropriate choice depends on the starting surface, the material being processed, the product geometry and the intended final appearance.
An abrasive that works well on a broad, flat handle may not be suitable for a curved spoon bowl or a narrow fork tine. Tool access, contact pressure and movement can differ significantly between these shapes.
A consistent finishing process should therefore define the relevant operating parameters and provide clear instructions for different product areas. These may include the abrasive sequence, tool condition, contact method and the criteria used to move from one finishing stage to the next.
Tool wear also deserves attention. As abrasive materials change through use, their performance may shift. Without appropriate monitoring, early and late production pieces can develop different surface characteristics even when the same general procedure is followed.
Manufacturers should select process settings based on validated production methods rather than applying one universal polishing formula to every cutlery design.
Protecting Product Geometry During Polishing
Polishing removes or refines surface material, so the process must preserve important design features. This is particularly relevant for spoon bowls, fork tines, knife blades and handles with narrow decorative details.
For spoons, excessive or uneven polishing can alter the appearance of the bowl or reduce the definition of its transitions. On forks, attention is needed around tine edges, gaps and the connection between the head and handle. On table knives, polishing should not unintentionally change the specified blade profile or soften important design lines.
A useful control plan identifies sensitive areas before production begins. The team can then determine which surfaces require special handling, which dimensions should be rechecked after finishing and which visual details must remain clearly defined.
For custom flatware, the product drawing should reflect the approved design, while the finishing instructions explain how that design should be maintained during processing. This connection helps prevent a visually attractive surface from being achieved at the expense of the original geometry.
Establishing a Repeatable Finishing Standard
A finishing standard should describe the intended result and the checks used to confirm it. General phrases such as “high-quality polish” do not provide enough detail for consistent evaluation across different teams or production batches.
A practical specification may include:
-
Finish type, such as mirror, satin or directional brushed.
-
Reference sample or approved finish photographs.
-
Areas requiring different surface treatments.
-
Acceptable visibility of polishing marks under agreed inspection conditions.
-
Requirements for preserving edges, contours and decorative details.
-
Inspection frequency and documentation for production batches.
These requirements should be adapted to the product rather than copied from a different cutlery collection. The surface characteristics that matter most on a premium retail handle may differ from those emphasized in a high-volume foodservice order.
The buyer and manufacturer should also agree on how borderline results will be reviewed. An agreed sample and documented criteria make these decisions more consistent than relying on individual preference.
Inspecting Polishing Results Across Bulk Production
A single approved sample demonstrates the target finish, but it does not prove that every bulk production batch will match it. Ongoing checks help confirm that the finishing process remains stable.
Inspection can include visual review under consistent lighting, comparison with the approved sample and closer examination of areas that are especially sensitive to reflection or abrasive marks. Where the product specification requires it, additional measurements may be used to check that polishing has not affected critical dimensions.
Records should identify the product SKU, production batch, observed issue and corrective action where applicable. If similar marks repeatedly appear in the same location, the factory can investigate the relevant operation instead of treating each piece as an isolated problem.
For a collection containing several spoon, fork and knife designs, the inspection plan should consider their different geometries. A broad spoon bowl may reveal uneven reflection differently from a narrow handle or a brushed knife blade. Product-specific checks are therefore useful even when all items share the same general finish.
Example: Maintaining a Coordinated Private Label Collection
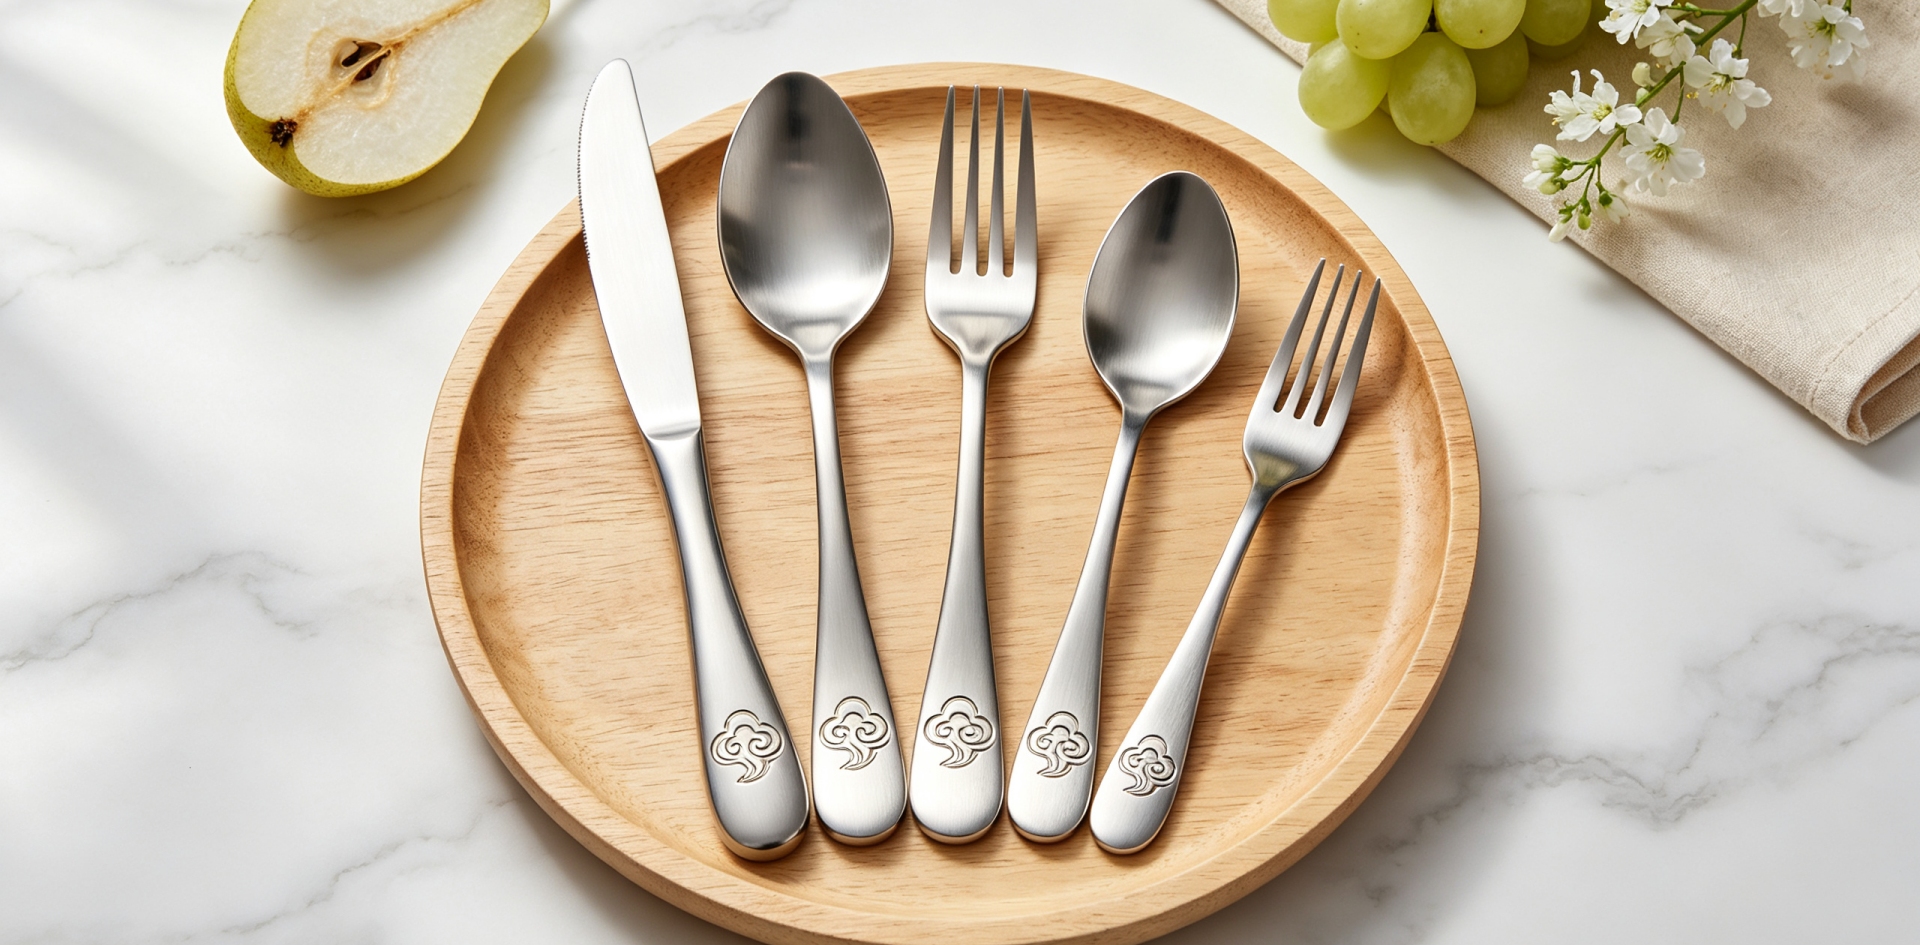
Consider a buyer developing a private label cutlery collection with dinner forks, tablespoons, teaspoons and table knives. The pieces use a similar handle design, but the spoon bowls and knife blades require different finishing treatments.
If each SKU is polished without a shared reference, the handles may develop different levels of gloss. The bowl of a tablespoon may appear more reflective than the smaller spoon, while the knife handle may show a different grain direction from the forks.
A coordinated finishing plan can address these risks by defining the common handle appearance, specifying the appropriate finish for each functional area and using the same agreed evaluation conditions. During sample approval, the buyer can review the complete collection together rather than judging each item in isolation.
This example illustrates why polishing consistency is a collection-level issue as well as an individual-product requirement.
How Homefelt Supports Finishing Requirements for OEM Orders
Homefelt factory supports stainless steel cutlery customization, OEM and ODM manufacturing, private label projects, wholesale supply and large-volume orders. For each project, the finishing plan can be discussed alongside material selection, product dimensions, logo treatment and packaging requirements.
Homefelt has experience in stainless steel cutlery manufacturing and has business credentials that include BSCI, SEDEX 4P, BRC and ISO 9001 audit or certification experience, together with Disney audit experience. FAMA and FSC certificates are available for applicable projects. Buyers can confirm which credentials and documents are relevant to the specific factory, product and order.
For projects that require closer finish control, buyers should provide reference samples, product drawings, target quantities and details of the intended application. These inputs help establish a realistic specification before production begins.
Homefelt can also coordinate product design, packaging and transportation as part of a one-stop service. Aligning the finishing requirements with the broader project plan supports clearer communication from sample development through bulk delivery.
Checklist Before Approving the Polishing Process
Before authorizing mass production, confirm that:
-
The required surface finish is defined by an approved reference.
-
The polishing sequence is suitable for the product's shape and material.
-
Abrasive tools and process settings are controlled for the relevant surfaces.
-
Sensitive contours, edges and decorative details are protected.
-
Inspection conditions and acceptance criteria are agreed upon.
-
Production records can identify recurring defects by SKU and batch.
-
Corrective actions are checked before the affected process continues.
These steps help buyers move beyond subjective descriptions and create a practical basis for consistent finishing. They also help manufacturers focus attention on the process stages that most strongly influence the final appearance.
You May Be Interested In
Stainless Steel Cutlery Production Lot Control for OEM and Wholesale Orders
Stainless Steel Cutlery Dimensional Deviation Control for OEM and Bulk Orders
Related Article